
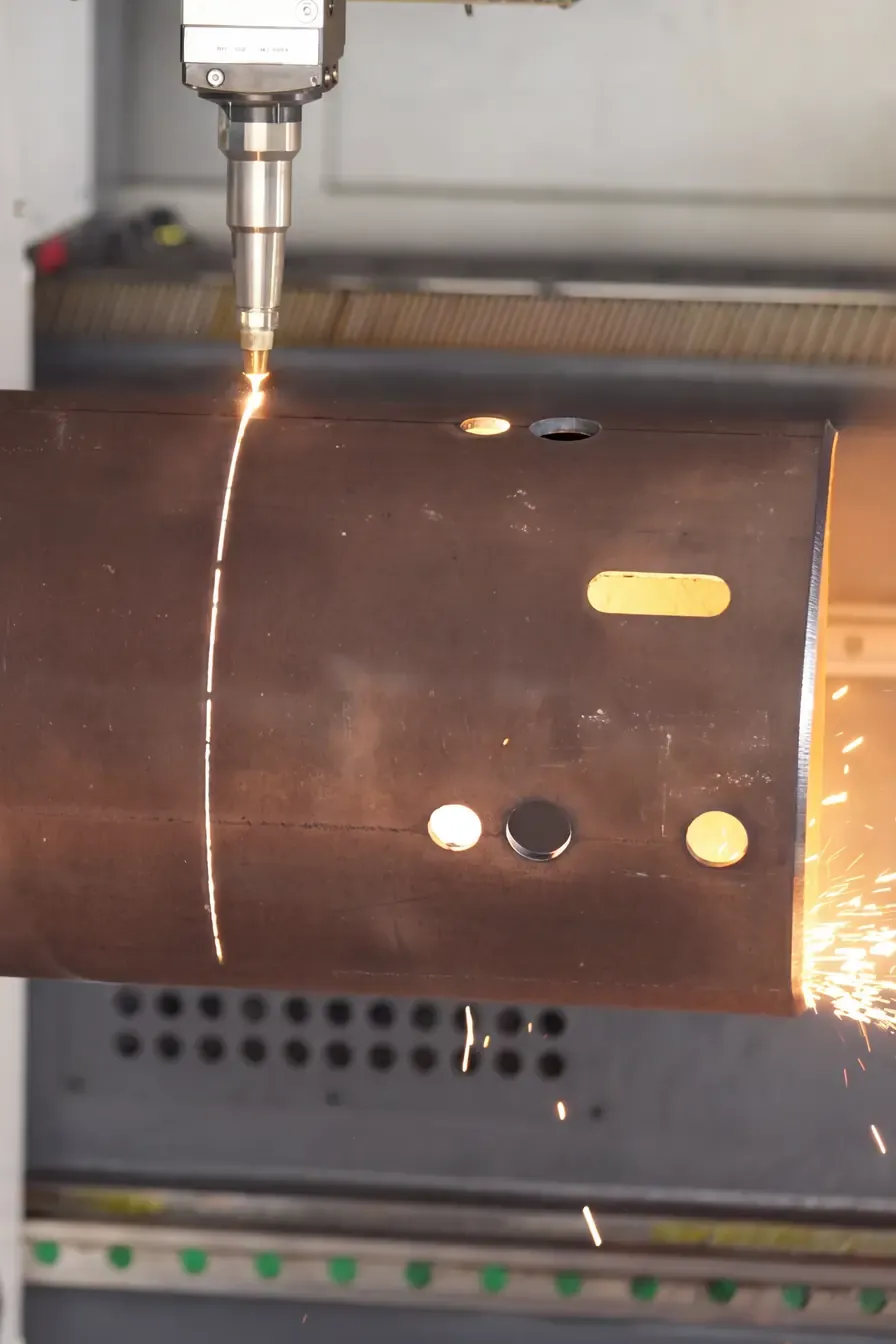
A tube is only finished when it fits the next part. Holes, slots, notches and end profiles cut by laser on the tube itself replace marking, drilling and grinding by hand, and they arrive repeatable from the first tube to the last.
Features that save time later
- Holes and slots: round holes, slotted holes and rectangular openings cut in one setup, positioned from your drawing or model.
- Notches and end profiles: saddle and angled ends for tube-to-tube joints, cut to the profile instead of fitted by grinding.
- Slots and tabs: where the design allows, tabs and matching slots help parts locate each other before welding, which shortens bench fit-up.
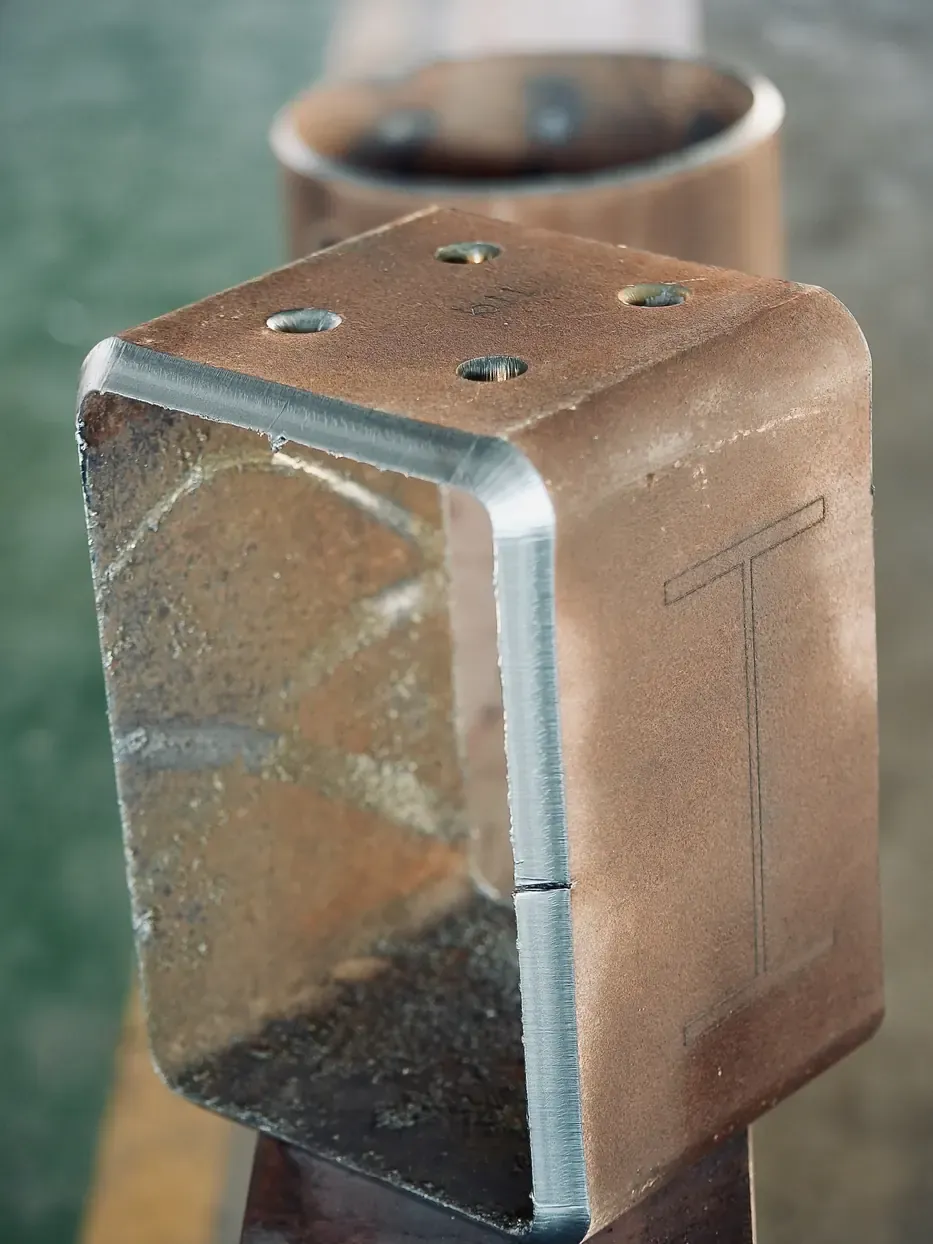
- Weld preparation: bevelled ends up to 45 degrees where the joint needs them.
Sizes and shapes
Round tube up to Ø650 mm, and square or rectangular tube within a 650 mm diagonal, in lengths up to 12 m.
What helps the fit-up
- Give the outside diameter or section size and the wall thickness.
- Mark which holes and slots are datum features for assembly.
- Show the mating part for any notch or end profile.
- Say which ends are welded and which are bolted.
Tubes continue to CNC bending, MIG or laser welding and finishing in the same Dubai Industrial City workshop. Send your tube drawings or STEP files or call +971 4 566 7219. See also steel fabrication in Dubai.